In the realm of modern agriculture, precision and reliability are paramount for optimizing harvesting operations. The Harvester GM100 Proximity Sensor stands as a critical component in this landscape, designed to enhance the performance and durability of harvesting machinery. This sensor is engineered to detect the presence or absence of objects without physical contact, utilizing electromagnetic fields to monitor the position of moving parts such as cutting blades, conveyors, and separators. Its robust construction ensures resilience against harsh environmental conditions, including dust, moisture, and temperature fluctuations commonly encountered in agricultural settings.
The GM100 sensor operates on the principle of inductive sensing, making it ideal for metallic targets. It features a high switching frequency and a sensing range tailored for agricultural applications, allowing for real-time adjustments in harvester functions. This capability minimizes downtime by preventing mechanical jams and optimizing the flow of harvested crops. For instance, when integrated into a combine harvester, the sensor can monitor the reel speed or the position of the header, ensuring seamless operation and reducing the risk of crop loss.
Key technical specifications include a supply voltage range of 10-30V DC, IP67 protection rating for dust and water resistance, and an operating temperature range of -25°C to 70°C. These attributes make the GM100 suitable for continuous use in demanding field conditions. Additionally, its compact design facilitates easy installation and maintenance, aligning with the need for minimal intervention during peak harvesting seasons.
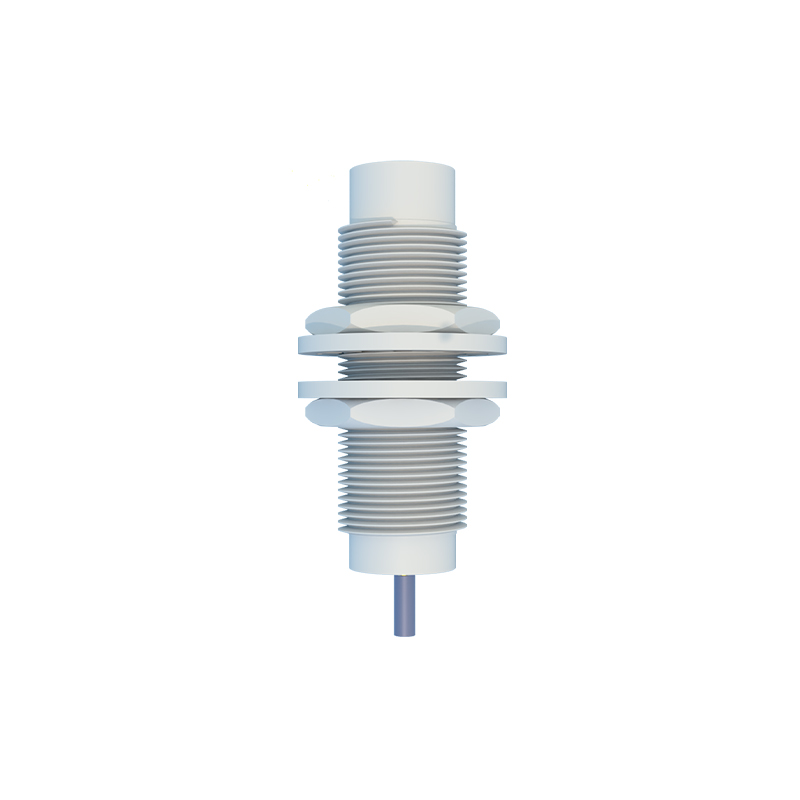
From an engineering perspective, the GM100 contributes to energy efficiency by enabling precise control over hydraulic and electrical systems. By providing accurate feedback, it helps regulate engine load and reduce fuel consumption, thereby lowering operational costs. Furthermore, its compatibility with various harvester models and control systems enhances versatility, allowing farmers to upgrade existing equipment without extensive modifications.
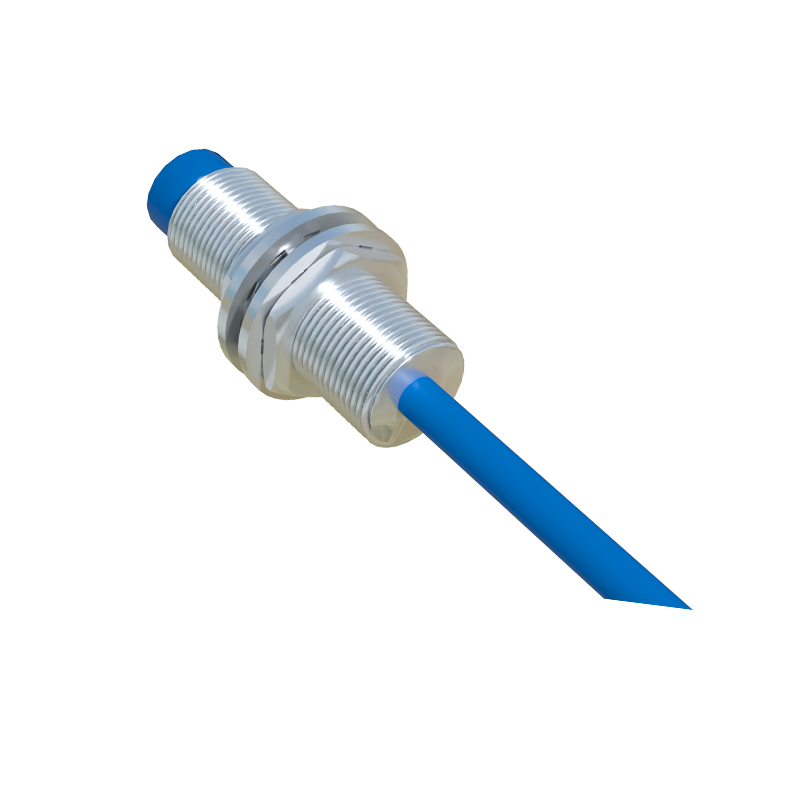
In practice, the implementation of GM100 proximity sensors has shown significant improvements in harvest quality and yield. For example, in grain harvesting, sensors ensure optimal cutting height and threshing efficiency, leading to cleaner grain separation and reduced waste. Testimonials from agricultural operators highlight increased machine uptime and decreased maintenance expenses, underscoring the sensor's role in sustainable farming practices.
Looking ahead, advancements in sensor technology may integrate the GM100 with IoT platforms for predictive maintenance and data analytics. This evolution could enable remote monitoring of harvester performance, alerting operators to potential issues before they escalate. As agriculture continues to embrace automation, the GM100 proximity sensor remains a foundational element in driving efficiency, safety, and productivity in harvesting operations worldwide.