In the rapidly evolving landscape of industrial automation, the 1100 series laser sensor stands as a pivotal component, driving advancements in precision measurement, quality control, and process optimization. Engineered to deliver exceptional accuracy and reliability, these sensors utilize advanced laser triangulation or time-of-flight principles to detect, measure, and monitor objects with micron-level precision. The core technology involves emitting a focused laser beam toward a target; the reflected light is then captured by a high-resolution receiver. By analyzing the displacement or phase shift of the returned signal, the sensor calculates exact distances, dimensions, or presence, even in challenging environments with variable surfaces, colors, or ambient light conditions.
The 1100 laser sensor is renowned for its robust design, typically featuring IP67 or higher ingress protection, making it suitable for harsh industrial settings such as manufacturing floors, automotive assembly lines, and logistics hubs. Its compact form factor allows for easy integration into existing machinery, while programmable parameters enable customization for specific tasks like edge detection, thickness gauging, or fill-level monitoring. With response times in the microsecond range, it supports high-speed production lines without compromising accuracy, thereby reducing downtime and minimizing material waste.
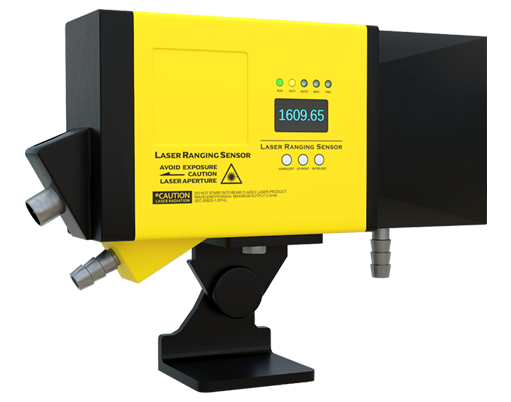
Key applications span diverse sectors. In automotive manufacturing, 1100 sensors ensure precise alignment of components during assembly, enhancing safety and performance. In packaging industries, they verify label placement and container integrity, maintaining brand consistency. Electronics manufacturers rely on them for solder paste inspection and component positioning, critical for miniaturized devices. Additionally, in logistics, these sensors facilitate automated sorting and inventory management by detecting parcel dimensions and tracking movements on conveyor belts.
The integration of smart features, such as IO-Link connectivity and real-time data output, allows the 1100 sensor to interface seamlessly with PLCs (Programmable Logic Controllers) and IoT (Internet of Things) networks. This enables predictive maintenance, where sensor data analytics can forecast potential failures before they occur, optimizing operational efficiency. Energy efficiency is another hallmark, with low-power designs that align with sustainable industrial practices.
Despite its advantages, users must consider factors like environmental interferences—e.g., dust, steam, or reflective materials—which may require complementary accessories like air purging units or specialized filters. Regular calibration and adherence to manufacturer guidelines ensure long-term performance. As Industry 4.0 accelerates, the 1100 laser sensor continues to evolve, with future iterations likely incorporating AI-driven analytics for adaptive sensing and enhanced autonomy.
In summary, the 1100 laser sensor exemplifies innovation in industrial sensing, offering a blend of precision, durability, and versatility. By enabling automated systems to perceive and react with exactitude, it underpins modern manufacturing’s shift toward smarter, more resilient operations. Professionals seeking to upgrade their automation toolkit should evaluate its specifications against application needs, ensuring optimal ROI through improved quality and productivity.