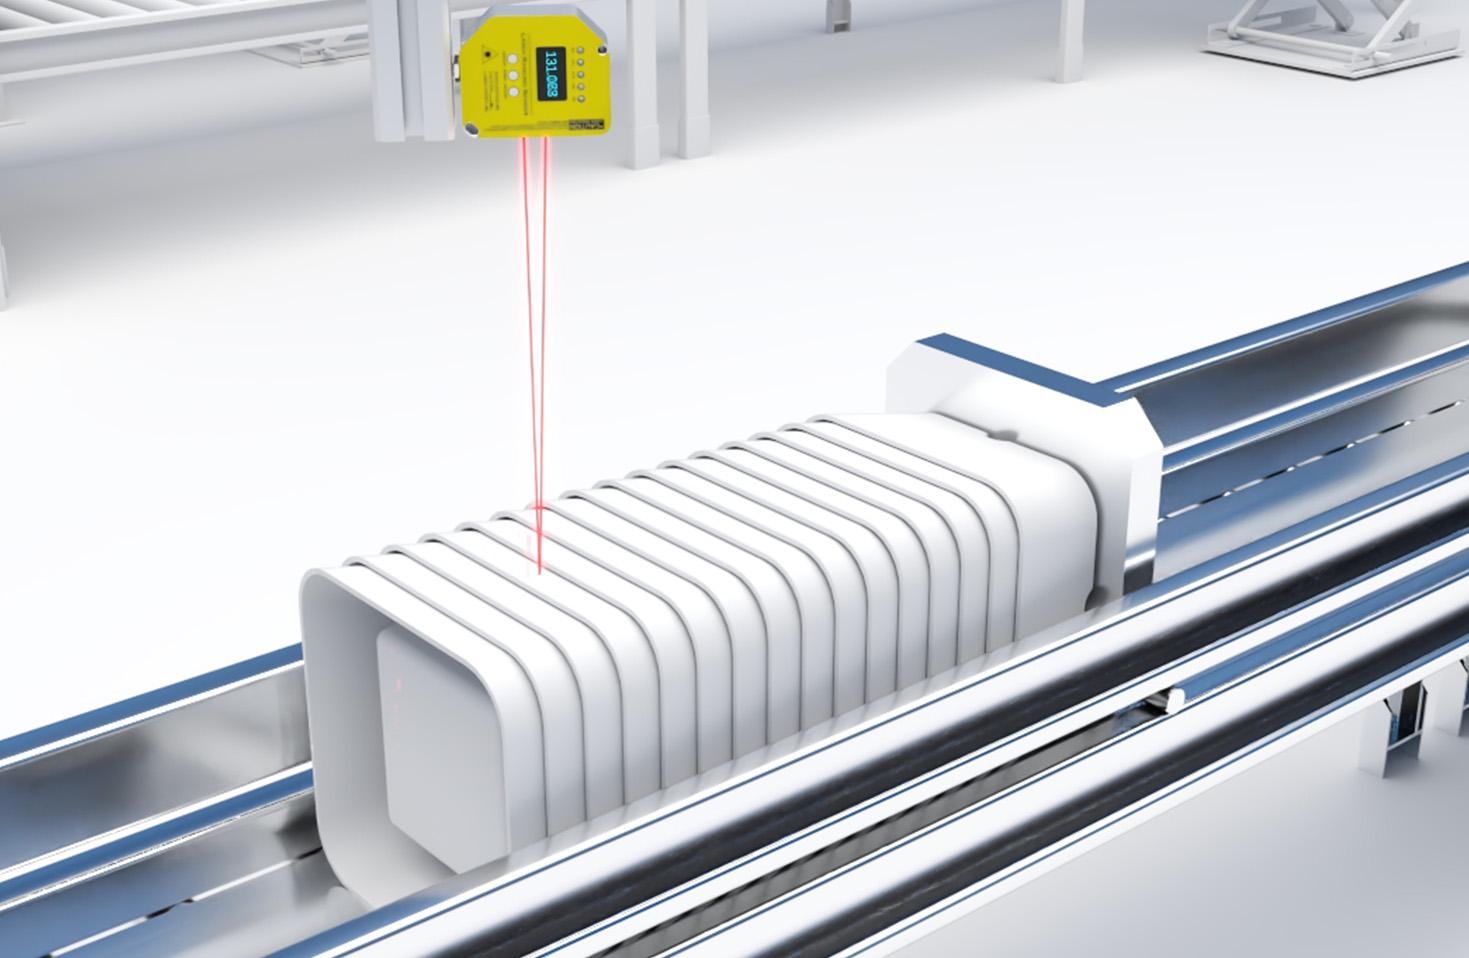
In the rapidly evolving landscape of industrial automation and precision measurement, the 150-meter laser sensor stands as a pivotal technology, enabling accurate, non-contact detection over significant distances. This article delves into the operational principles, core applications, and critical selection criteria for these advanced sensing devices, providing essential insights for engineers and system integrators.
At its core, a 150-meter laser sensor operates on the principle of time-of-flight (ToF) or phase-shift measurement. The sensor emits a modulated laser beam towards a target. The beam reflects off the target's surface and returns to the sensor's receiver. By precisely measuring the time delay or phase difference between the emitted and reflected signals, the sensor calculates the distance to the target with high accuracy. This method allows for reliable operation even at the full 150-meter range, under suitable environmental conditions. Key components include a high-power, eye-safe laser diode (typically in the infrared spectrum), a sensitive photodetector, and sophisticated signal processing circuitry that filters out ambient light and noise.
The performance of these long-range sensors is characterized by several critical parameters. The measuring range is explicitly up to 150 meters, though effective range can be influenced by target reflectivity and environmental factors. Accuracy and resolution are paramount; high-end models offer sub-millimeter accuracy and resolution, even at maximum distance. The response time, or measurement frequency, determines how quickly the sensor can update distance readings, which is crucial for dynamic applications like vehicle guidance or fast-moving objects. Furthermore, the laser spot size increases with distance, affecting measurement precision on small targets. Engineers must also consider the ingress protection (IP) rating for dust and water resistance, operational temperature range, and communication interfaces (e.g., analog outputs, Ethernet, PROFINET, IO-Link).
The applications for 150-meter laser sensors are diverse and transformative across multiple sectors. In logistics and warehousing, they are indispensable for inventory profiling, measuring stockpile volumes in large yards, and guiding automated guided vehicles (AGVs) in expansive facilities. The construction and mining industries leverage them for monitoring excavation depths, measuring stockpile volumes of bulk materials like coal or ore, and ensuring the safe operation of large machinery. In port automation, these sensors facilitate the positioning of shipping containers and assist crane systems. Additionally, they play a role in security and perimeter protection, creating invisible detection fences over long distances. Their ability to perform reliably in harsh environments—withstanding dust, vibration, and variable lighting—makes them superior to traditional ultrasonic or shorter-range optical sensors for these demanding tasks.

Selecting the appropriate 150-meter laser sensor requires a meticulous analysis of the application's needs. The primary consideration is the target properties: its color, surface texture, and reflectivity. A dark, matte, or absorbing surface will return a weaker signal than a bright, reflective one, potentially reducing the effective range. Some sensors feature automatic sensitivity adjustment or multiple echo processing to handle difficult surfaces. Environmental conditions are equally critical. Outdoor applications must account for direct sunlight, rain, fog, and temperature extremes. Sensors with robust housings, high IP ratings (e.g., IP67), and built-in environmental compensation algorithms are essential for reliable outdoor use. The required measurement profile—whether continuous distance monitoring, single-point triggering, or area scanning—will dictate the choice of sensor model. Finally, integration ease, including mounting options, configuration software, and compatibility with existing control systems (PLCs), is a practical necessity for seamless deployment.
In conclusion, the 150-meter laser sensor is a powerful tool that extends the capabilities of automated systems by providing precise, long-range distance data. Its technology, based on robust optical time-of-flight principles, meets the rigorous demands of modern industry. Successful implementation hinges on a thorough understanding of both the sensor's specifications and the specific challenges of the application environment. As industries continue to push for greater efficiency, safety, and autonomy, the role of long-range laser measurement technology will only become more central, driving innovation in large-scale automation and control systems.