Photo laser sensors, a cornerstone of modern industrial automation, operate on the fundamental principles of optical triangulation and time-of-flight (ToF) measurement. These non-contact devices emit a focused laser beam toward a target object. The core operational methodology diverges into two primary, widely adopted techniques.
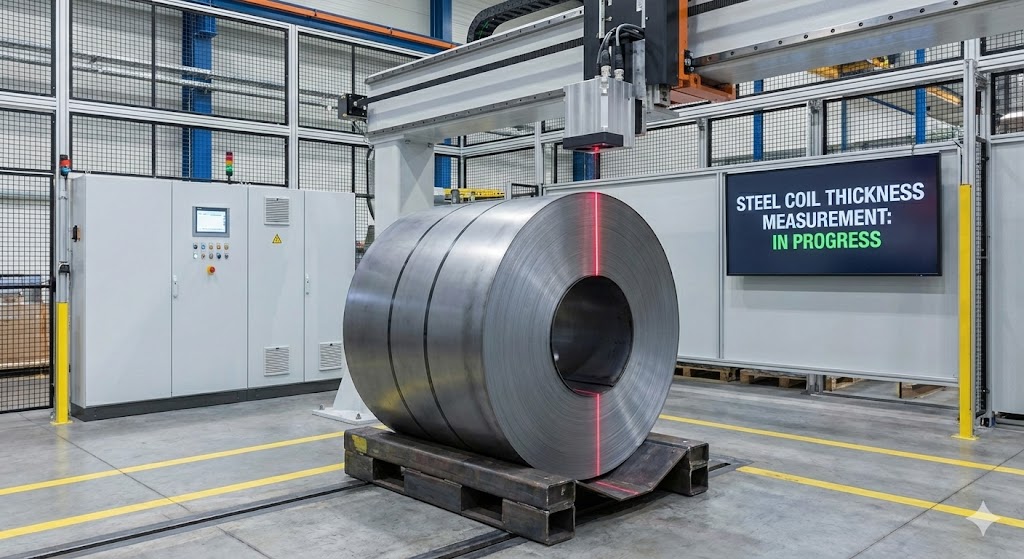
The first and most common principle for short to medium-range applications is laser triangulation. In this method, the sensor's transmitter projects a visible or infrared laser dot onto the target surface. The diffuse reflection from this point is then captured by a precision receiver element, typically a Position-Sensitive Detector (PSD) or a Charge-Coupled Device (CCD) array. The key to measurement lies in the geometric relationship. As the distance to the target changes, the angle of the reflected light entering the receiver lens shifts. This causes the position of the laser spot image on the detector to move proportionally. The sensor's internal microprocessor calculates the exact distance or presence by analyzing this positional shift with high-speed algorithms. This principle offers exceptional accuracy for tasks like height profiling, thickness measurement, and precise object detection on assembly lines.
For longer ranges or where high-speed distance measurement is critical, the Time-of-Flight (ToF) principle is employed. Here, the sensor emits modulated laser pulses. A high-speed clock circuit measures the precise time interval between the emission of a pulse and the detection of its reflection. Since the speed of light is a known constant, the distance to the target is calculated directly using the formula: Distance = (Speed of Light × Time Delay) / 2. Advanced ToF sensors use phase-shift measurement of continuous wave modulation for even greater resolution. This technology is ideal for applications such as bulk level sensing in silos, vehicle detection in logistics, and large-area object positioning.
Beyond distance measurement, the operational logic of photo laser sensors is defined by their output configuration. The analog output provides a continuous voltage or current signal proportional to the measured distance, enabling precise positional feedback. The digital output, often via NPN/PNP transistors or push-pull circuits, provides a discrete ON/OFF signal triggered when a target enters or exits a pre-set sensing window. This programmability allows for versatile use in counting, edge detection, and automated quality control gates.
Environmental robustness is a critical design consideration. Industrial environments present challenges like ambient light interference, dust, steam, and vibrations. Engineers mitigate these through several means: using lasers with specific wavelengths and narrow-band optical filters to reject ambient light, incorporating robust housings with high Ingress Protection (IP) ratings, and implementing advanced algorithms for background suppression and signal averaging. The choice between a red visible laser for easy alignment and an infrared laser for covert operation or better performance in certain materials is also an application-specific decision.
In practice, the integration of these sensors into a control system is seamless. They communicate via standard interfaces like IO-Link, which provides detailed parameterization and diagnostic data, or analog/digital signals to Programmable Logic Controllers (PLCs). Calibration involves teaching the sensor the reference positions for the near and far points of its sensing range. Regular maintenance primarily involves keeping the lens clean to ensure optimal signal strength and accuracy.
From ensuring robotic arms pick components at the exact correct height to verifying the fill level of transparent bottles on a high-speed packaging machine, photo laser sensors provide the reliable, micron-level precision that automated systems demand. Their continued evolution, incorporating features like multi-point measurement and integrated evaluation, solidifies their role as indispensable eyes for industrial machinery.