In modern industrial automation, labeling machines play a critical role in product identification, traceability, and branding across sectors like food and beverage, pharmaceuticals, cosmetics, and logistics. At the heart of these systems' precision and reliability are laser sensors, specifically laser photoelectric sensors used for detection and positioning. Unlike traditional mechanical or pneumatic sensors, laser sensors offer non-contact, high-accuracy sensing capabilities essential for high-speed production lines.
Laser sensors in labeling machines primarily function as object detection and edge-positioning devices. They emit a focused laser beam—typically red or blue visible light—toward a target. When the beam strikes an object, such as a product on a conveyor, the reflected light is captured by the sensor's receiver. Based on the intensity or time-of-flight of the returned signal, the sensor determines the presence, absence, or precise position of the item. This triggers the labeling head to apply a label at the exact required location. Common configurations include through-beam sensors, where the emitter and receiver are separate units, and reflective sensors, which use a reflector or the object itself to bounce light back.
The advantages of laser sensors are manifold. First, their high precision, with detection resolutions down to sub-millimeter levels, ensures labels are placed consistently even on small or irregularly shaped items. Second, laser beams are highly visible and can be finely adjusted, simplifying alignment during installation and maintenance. Third, they are less susceptible to environmental interference like ambient light or dust compared to some optical sensors, though this depends on the model and housing rating (e.g., IP67 for washdown environments). Fourth, their fast response time, often in microseconds, supports high-speed operations without bottlenecks.
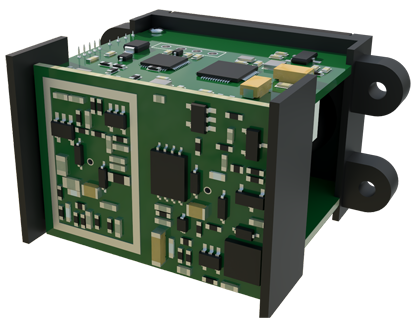
Key technical parameters to consider when selecting a laser sensor for labeling include sensing range, spot size, response time, output type (e.g., NPN/PNP, analog, or IO-Link), and environmental durability. For instance, in beverage labeling, a sensor with a 100-300mm range and high immunity to moisture is typical. Advanced sensors may feature teach-in functions for easy calibration or background suppression to ignore distant objects.
Integration into labeling systems involves mounting the sensor to detect products as they enter the labeling zone. The sensor signal is wired to the machine's PLC or controller, which coordinates the label dispenser. Proper alignment is crucial: the laser must strike the product at a consistent point. Regular maintenance includes lens cleaning to prevent residue buildup from affecting performance.
Applications vary widely. In pharmaceutical labeling, laser sensors ensure precise label placement on vials or blister packs for compliance. In logistics, they detect packages of different sizes to trigger print-and-apply labeling. Challenges can include handling transparent or glossy surfaces that reflect light poorly, which may require sensors with polarized filters or adjustable sensitivity.
Emerging trends involve smart sensors with networking capabilities, allowing real-time monitoring and predictive maintenance via industrial IoT. Additionally, miniaturized laser sensors enable compact labeling designs for space-constrained lines.
In summary, laser sensors are indispensable for modern labeling machines, delivering the accuracy and speed demanded by today's industries. By understanding their operation and selection criteria, engineers can optimize labeling processes for efficiency and quality. Always refer to manufacturer guidelines and conduct thorough testing to ensure optimal performance in specific applications.