Proximity sensors are indispensable components in modern industrial automation, offering non-contact detection capabilities that enhance efficiency, safety, and reliability. These sensors operate by emitting an electromagnetic field or a beam of radiation, such as infrared light, and detecting changes in the field or return signal when an object enters their sensing range. Unlike mechanical switches, proximity sensors do not require physical contact, which minimizes wear and tear, reduces maintenance needs, and extends operational lifespan.
One primary function of proximity sensors is object detection and positioning. In manufacturing lines, they accurately identify the presence, absence, or position of items like metal parts, containers, or products on conveyor belts. For instance, inductive proximity sensors excel at detecting metallic objects by generating an eddy current in the target, while capacitive sensors can sense non-metallic materials such as plastics, liquids, or wood. This versatility allows for precise control in assembly processes, packaging, and material handling, ensuring smooth operations without interruptions.
Another critical function is speed and motion monitoring. Proximity sensors measure rotational speed or linear movement by detecting gear teeth, encoder discs, or other moving components. In automotive or machinery applications, they provide real-time data for controlling motor speeds, preventing overloads, and synchronizing operations. This capability is vital for maintaining consistent performance in systems like robotic arms, CNC machines, and automated guided vehicles (AGVs), where timing and accuracy are paramount.
Safety is a paramount concern in industrial settings, and proximity sensors contribute significantly to this area. They serve as safety devices by monitoring hazardous zones or machinery guards. For example, magnetic proximity sensors can detect if a protective door is properly closed, while ultrasonic sensors monitor distances to prevent collisions in automated systems. By triggering alarms or shutting down equipment when unsafe conditions are detected, these sensors help prevent accidents, protect workers, and comply with safety regulations like ISO 13849.
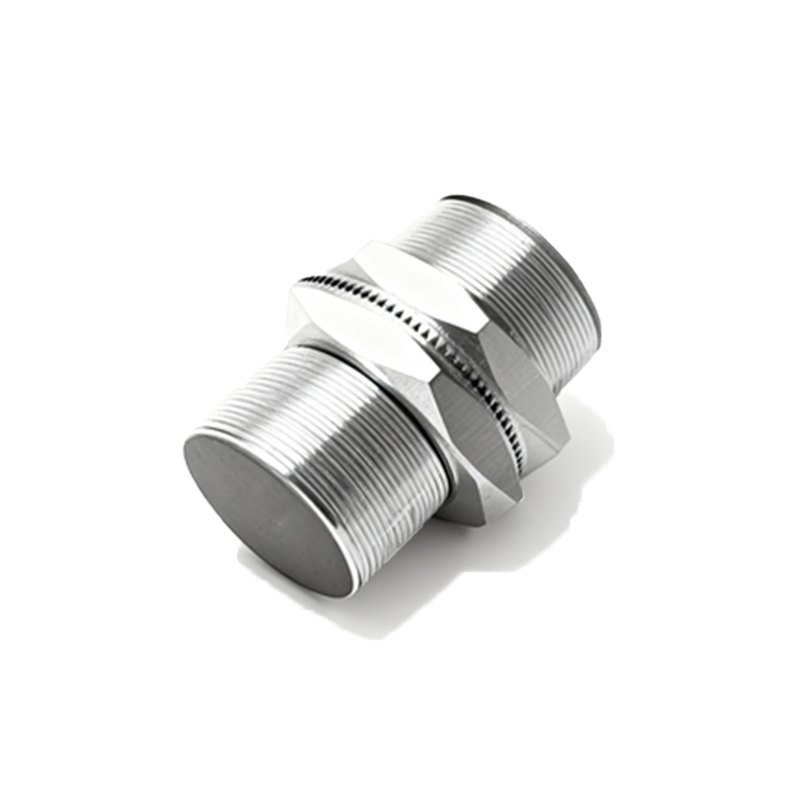
Additionally, proximity sensors aid in quality control and inspection. In high-precision industries, such as electronics or pharmaceuticals, they verify component placement, measure dimensions, or check for defects without physical contact. Photoelectric proximity sensors, which use light beams, are particularly effective for detecting transparent or small objects, ensuring products meet stringent quality standards. This function reduces waste, improves product consistency, and supports lean manufacturing principles.
Energy efficiency is another benefit offered by proximity sensors. By activating machinery only when needed—such as turning on lights when a person approaches or starting a conveyor when a product is detected—they reduce power consumption and operational costs. In smart buildings or IoT-enabled systems, proximity sensors integrate with control networks to optimize resource use, contributing to sustainable practices.
In summary, proximity sensors perform diverse functions including object detection, positioning, speed monitoring, safety enhancement, quality control, and energy management. Their non-contact nature, durability, and adaptability make them essential for advancing industrial automation. As technology evolves, innovations like IoT integration and AI-driven analytics are expanding their roles, enabling smarter, more responsive systems. For engineers and industry professionals, understanding these functions is key to leveraging proximity sensors for improved productivity and innovation.