In modern industrial manufacturing, the quality and consistency of raw materials directly impact the final product's performance, safety, and cost-efficiency. Traditional inspection methods, such as manual sampling or contact-based measurement, often fall short in terms of speed, accuracy, and scalability. This is where laser sensor technology emerges as a transformative solution for raw material inspection, offering non-contact, high-precision, and real-time analysis capabilities that are revolutionizing quality control processes across sectors like metals, polymers, ceramics, and composites.
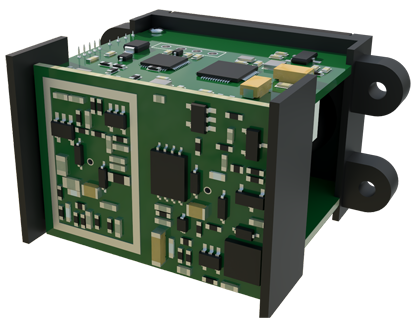
Laser sensors operate on principles of optical triangulation, time-of-flight, or interferometry, emitting focused laser beams onto material surfaces. The reflected or scattered light is captured by detectors, enabling precise measurement of physical properties such as thickness, density, surface roughness, and compositional uniformity. For instance, in metal production, laser-based systems can detect microscopic cracks, inclusions, or dimensional deviations in raw billets or sheets with micron-level accuracy, preventing downstream processing failures. In polymer manufacturing, sensors analyze melt flow index or color consistency by evaluating light absorption and scattering patterns, ensuring batch-to-batch uniformity.
The core advantages of laser sensors in raw material inspection include their non-destructive nature, which preserves material integrity, and their ability to operate in harsh environments—high temperatures, dust, or vibrations—where human inspectors or conventional tools may fail. Advanced systems integrate machine learning algorithms to interpret sensor data, identifying defects or anomalies that might be invisible to the naked eye. For example, hyperspectral laser sensors can assess chemical composition by analyzing wavelength-specific reflections, crucial for verifying alloy grades or detecting contaminants in pharmaceutical powders.
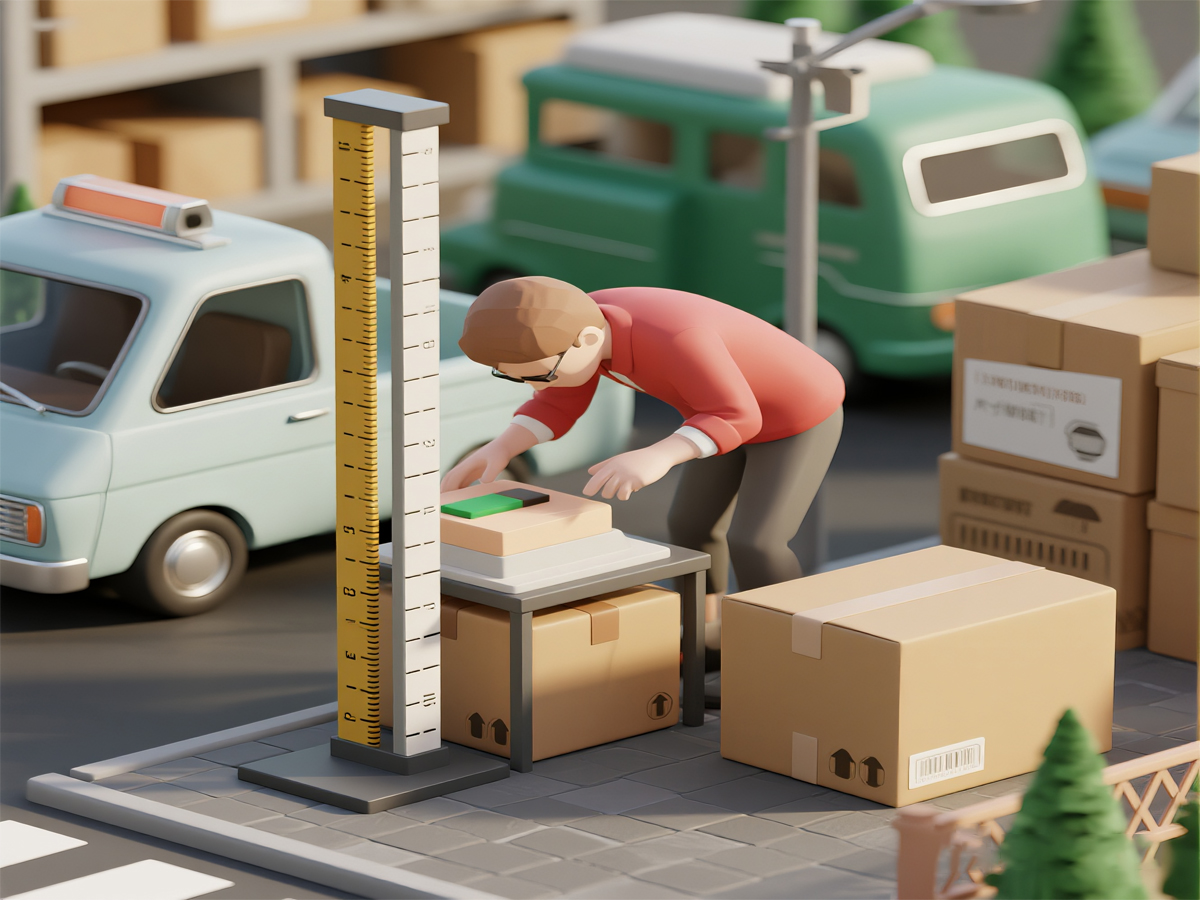
Implementation typically involves integrating laser sensors into production lines, such as conveyor belts or robotic arms, for continuous monitoring. Data from sensors feed into centralized control systems, enabling automated adjustments or alerts for non-conforming materials. This not only reduces waste and rework but also enhances traceability, as each material batch can be logged with detailed inspection records. In industries like automotive or aerospace, where material specifications are stringent, laser inspection ensures compliance with international standards like ISO or ASTM, mitigating risks of structural failures.
Despite their benefits, challenges exist, including initial investment costs, calibration requirements, and sensitivity to extreme surface conditions (e.g., highly reflective or transparent materials). However, ongoing advancements in fiber lasers, miniaturized sensors, and AI-driven analytics are making these systems more accessible and robust. Future trends point toward IoT-enabled laser networks for predictive maintenance and sustainability-driven applications, such as optimizing raw material usage to minimize environmental impact.
In summary, laser sensor technology represents a cornerstone of Industry 4.0, empowering manufacturers to achieve unprecedented levels of quality and efficiency in raw material inspection. By leveraging light-based precision, industries can foster innovation, reduce operational costs, and build resilient supply chains in an increasingly competitive global market.