Forget the pristine lab curves and idealized spec sheets. After two decades on factory floors, in dusty warehouses, and beside high-speed assembly lines, I can tell you that using laser sensors to detect plastics is a game of managing the unseen. The theory is straightforward—measure the reflection or transmission of a laser beam. The reality is a constant negotiation with environmental gremlins and material quirks that no manual fully prepares you for.
Experience Correction: The Dirty Truth About Specs
The most glaring deviation from theory is the assumed surface consistency. A polypropylene homopolymer and a copolymer might share the same name on a bill of lading, but their laser reflectivity can differ by over 40% due to filler content, pigment type (especially titanium dioxide levels), and surface texture from molding. I've seen a sensor calibrated for "clear ABS" fail consistently because the batch had a matte finish from a worn mold, scattering the laser beam. The published detection range? Cut it by 25-30% if your plastic part has any degree of translucency. The laser doesn't just bounce off; it penetrates and scatters internally, leading to a weak and noisy signal. In high-vibration environments (think injection molding machines or conveyor junctions), a sensor's stated repeatability of ±0.1mm is fantasy. Real-world thermal drift from motor heat and mechanical shock will push that to ±0.5mm or worse, unless you're using actively temperature-compensated models and military-grade mounting.
Boundary Conditions: When to Walk Away

Laser sensors are not universal tools. Knowing when *not* to use them is critical.
1. Highly Glossy or Mirror-Finish Plastics: The specular reflection will direct the beam away from the receiver, causing a complete miss. This is especially perilous with clear, glossy films.
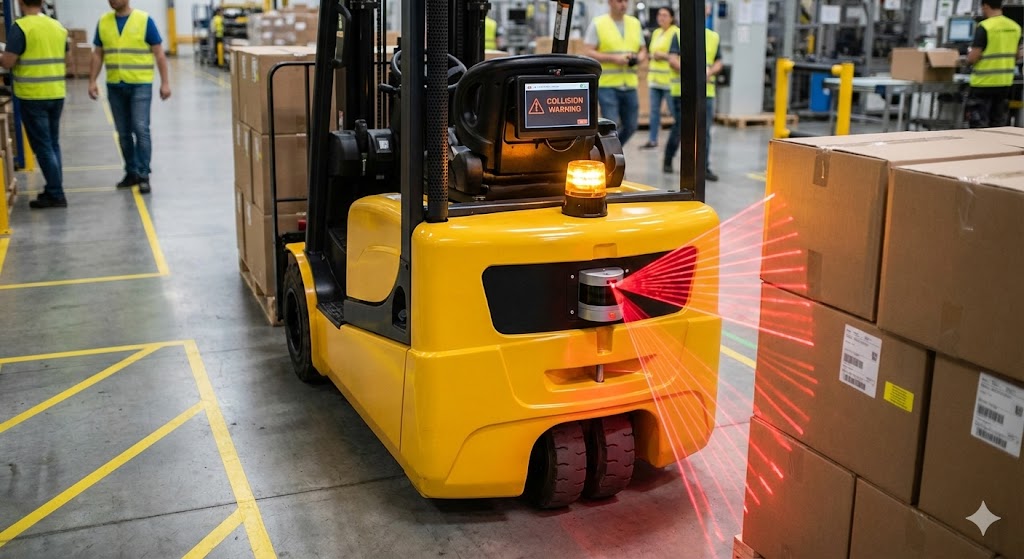
2. Ambient Light Saturation: Any application exposed to direct sunlight, arc welding, or high-intensity strobe lights (like from other inspection systems) is a hard no. Even the best modulated lasers can be drowned out. I witnessed a failure where a sensor reading black PVC was blinded intermittently by a forklift's headlight 20 meters away.
3. Rapid Color or Material Changes: If your line processes a random mix of black, white, and translucent plastics, a standard diffuse reflective sensor will require constant, manual re-teaching. It's unsustainable.
4. Presence of Dust, Steam, or Oil Mist: These particulates create a "fog" that attenuates the laser beam. A through-beam sensor might interpret heavy dust as an opaque object, triggering false positives. In such conditions, ultrasonic sensors or robust mechanical limit switches often prove more reliable, albeit less precise.
Counterintuitive Conclusion: Sometimes, a Weaker Laser is Better
Here’s the insight that contradicts procurement logic: a higher-power Class 2 or Class 3R laser is not always superior for plastic detection. In many cases, a low-power, red-light laser diode (Class 1) paired with a high-sensitivity, narrow-bandpass receiver yields more stable results. Why? Powerful lasers exacerbate the "subsurface scattering" effect in semi-crystalline plastics like HDPE or PP, creating a diffuse return signal that confuses the receiver's threshold logic. The intense beam can also cause localized heating on dark-colored plastics, potentially altering the surface slightly over millions of cycles and drifting the signal. Data from a long-term test on a bottle cap sorting line showed that a 0.8mW red laser sensor achieved a 99.98% detection rate on black caps, while a 5mW blue laser sensor started at 99.99% but degraded to 99.7% over six months, likely due to microscopic surface changes from minimal heat absorption. The pursuit of signal strength can ironically introduce the noise you're trying to avoid. The key is spectral matching and receiver sensitivity, not raw optical power.
Ultimately, success hinges on treating the laser sensor as a living component in a hostile ecosystem. Your calibration must account for the dirtiest part, the hottest ambient temperature, and the most problematic material variant. The goal isn't perfect detection in a controlled state, but predictable, manageable failure modes in an unpredictable world.