Revolutionizing Detection with Advanced LED Technology
The newly launched Ultra-Bright LED Proximity Sensor represents a significant leap forward in industrial automation and sensing solutions. Engineered for environments where reliability and precision are non-negotiable, this sensor utilizes cutting-edge LED technology to deliver unparalleled performance. Traditional sensors often struggle in challenging conditions such as extreme ambient light, dust, or varying surface reflectivities. However, the intense, focused beam of the ultra-bright LED overcomes these obstacles, ensuring consistent and accurate detection of objects, regardless of material or color. This innovation is not merely an incremental improvement but a foundational shift, providing engineers and system integrators with a tool that enhances machine efficiency and reduces false triggers, ultimately leading to higher productivity and lower operational costs.
Unmatched Performance in Demanding Environments
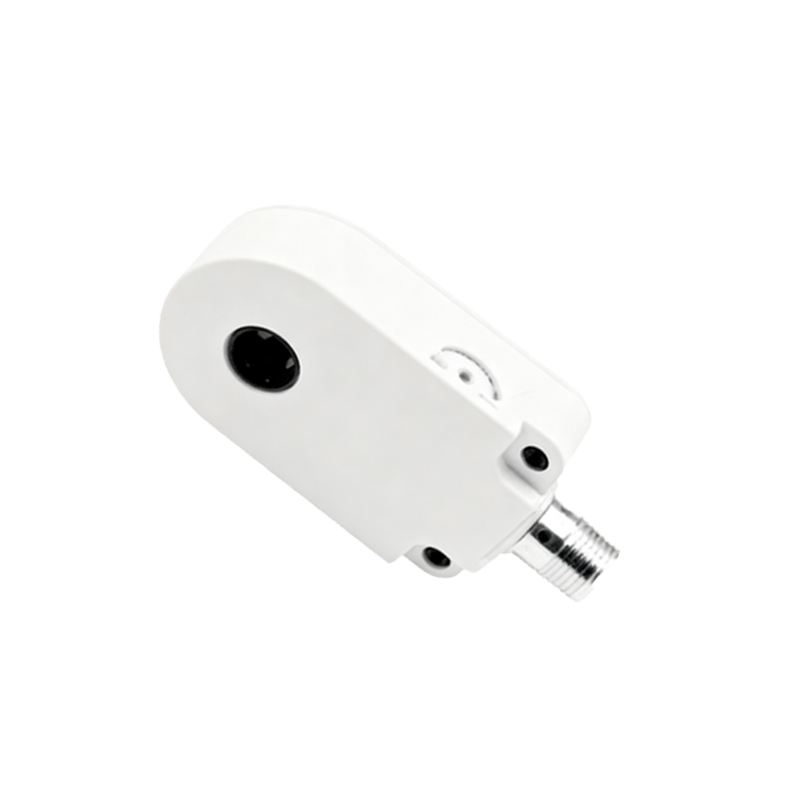
What sets this proximity sensor apart is its exceptional operational robustness. Designed to meet IP67 and IP69K ratings, it is fully protected against dust ingress and high-pressure water jets, making it ideal for harsh manufacturing floors, food processing plants, and outdoor applications. The sensor's housing is constructed from high-grade stainless steel and engineered polymers, ensuring durability against physical impacts and chemical exposures. Furthermore, its extended sensing range, achievable through the powerful LED output, allows for greater installation flexibility. Users can mount the sensor farther from the target, simplifying mechanical design and maintenance access. The consistent light output also minimizes drift over time and temperature fluctuations, a common pain point with older technologies, guaranteeing long-term stability and reducing the need for frequent recalibration.
Enhanced Connectivity and Smart Features
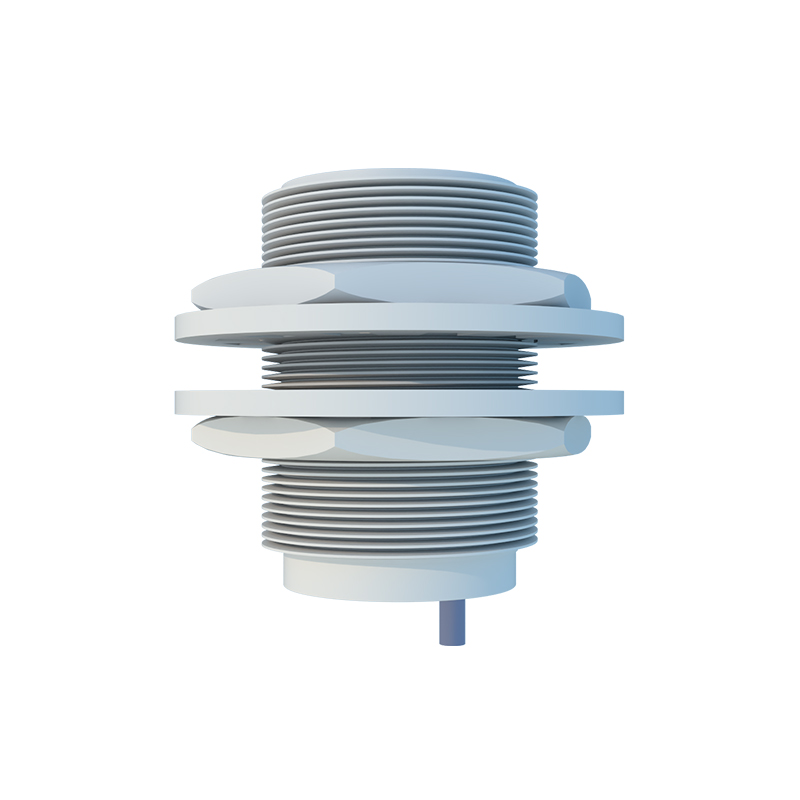
Integration into modern Industry 4.0 frameworks is seamless with the sensor's advanced connectivity options. It supports standard IO-Link communication, enabling detailed parameterization, real-time diagnostics, and predictive maintenance data exchange with central control systems. This digital interface allows for remote adjustment of sensing parameters, such as sensitivity and response time, without physical intervention at the sensor location. Additionally, the device features a clear, multi-status LED indicator that provides instant visual feedback on operational state, signal strength, and potential fault conditions. These smart capabilities empower maintenance teams to proactively address issues before they lead to downtime, transforming the sensor from a simple detection component into an intelligent node within a networked industrial ecosystem.
Energy Efficiency and Sustainable Operation
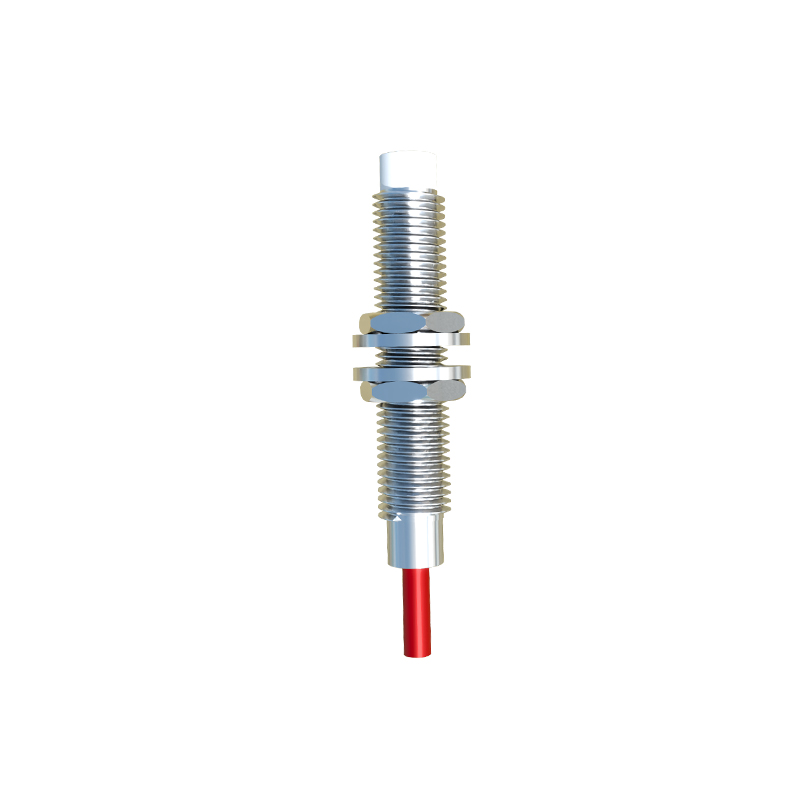
Despite its high output, the Ultra-Bright LED Proximity Sensor is engineered for optimal energy consumption. The LED technology itself is inherently more efficient than traditional incandescent or older semiconductor light sources, converting a higher percentage of electrical power into usable light with minimal heat generation. This efficiency translates directly into lower power draw from the control system, contributing to reduced overall energy costs for the facility. Moreover, the sensor's long operational lifespan—significantly exceeding that of conventional models—reduces waste from frequent replacements. By minimizing energy use and material waste, this product aligns with growing industrial sustainability goals, helping companies lower their carbon footprint while maintaining peak operational performance.
Broad Application Spectrum Across Industries
The versatility of this sensor opens doors for innovation across numerous sectors. In automotive assembly lines, it ensures precise part positioning and robotic guidance. In packaging machinery, it detects labels, fills, and seals with high speed and accuracy. The logistics and material handling industry benefits from its ability to reliably sense packages on high-speed conveyors, regardless of packaging color or reflectivity. Even in cleanrooms and electronic manufacturing, where contamination sensitivity is critical, the sensor's sealed design and precise beam control prevent interference with delicate processes. This wide applicability makes it a valuable, future-proof investment for any operation seeking to upgrade its sensing infrastructure for greater reliability and intelligence.
Commitment to Support and Technical Excellence
Launching this product is accompanied by a comprehensive support package designed to ensure successful deployment. This includes detailed technical documentation, CAD models for easy integration into machine designs, and access to a global network of application engineers. These experts provide guidance on selection, installation, and troubleshooting, helping customers maximize the sensor's value from day one. Continuous firmware updates, delivered via the IO-Link interface, will also ensure the sensor's features remain at the cutting edge, protecting the customer's investment over its long service life. This commitment underscores the philosophy that a superior product must be backed by superior support, fostering trust and long-term partnerships within the industrial community.