In modern industrial automation, the integration of Programmable Logic Controllers (PLCs) with laser sensors represents a pivotal advancement in precision control and monitoring. PLCs, as the brain of automated systems, rely on accurate input data from sensors to execute complex tasks. Laser sensors, known for their high accuracy, non-contact measurement, and reliability, are increasingly being interfaced with PLCs to enhance operational efficiency across various sectors, including manufacturing, packaging, and robotics.
The process of connecting a laser sensor to a PLC typically involves several key steps. First, selecting the appropriate laser sensor is crucial. Factors such as measurement range, resolution, response time, and environmental conditions (e.g., temperature, dust, or vibration) must be considered. Common types include diffuse reflective sensors, through-beam sensors, and distance-measuring sensors, each suited for specific applications. For instance, through-beam sensors are ideal for detecting objects in high-speed production lines, while distance-measuring sensors excel in positioning tasks.
Once the sensor is chosen, the electrical connection must be established. Most laser sensors output signals in digital (e.g., NPN or PNP) or analog (e.g., 0-10V or 4-20mA) formats. Digital outputs are often used for simple presence detection, sending a high or low signal to the PLC's input module when an object is detected. Analog outputs, on the other hand, provide continuous data, such as distance or thickness measurements, which can be processed by the PLC for real-time adjustments. Wiring should follow manufacturer guidelines, ensuring proper voltage levels (commonly 24V DC for industrial PLCs) and shielding to prevent electromagnetic interference.
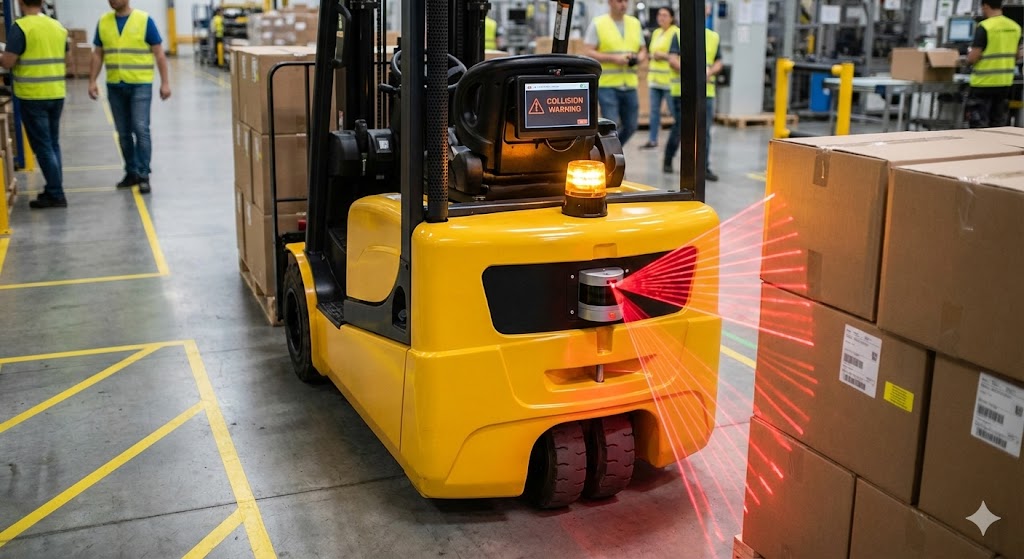
Programming the PLC to interpret sensor data is the next critical phase. Using ladder logic or structured text, engineers configure the PLC to read input signals from the sensor. For digital sensors, this may involve setting up routines to trigger actions—like activating a conveyor belt or stopping a machine—when the sensor detects an object. For analog sensors, scaling functions are employed to convert raw input values (e.g., from 0-4095 for a 12-bit analog module) into engineering units, such as millimeters or inches. Advanced PLCs also support communication protocols like PROFINET, EtherNet/IP, or Modbus, enabling seamless integration with smart laser sensors that offer networked capabilities for data logging and diagnostics.
The benefits of PLC-laser sensor integration are substantial. Enhanced precision reduces material waste and improves product quality, as seen in cutting or welding applications where laser sensors guide tools with micron-level accuracy. Increased automation speeds up processes, boosting throughput while minimizing human error. Moreover, predictive maintenance becomes feasible; by monitoring sensor data trends, PLCs can alert operators to potential issues, such as sensor misalignment or wear, before they cause downtime.
However, challenges exist. Environmental factors like ambient light or reflective surfaces can interfere with laser sensors, requiring careful installation and calibration. Compatibility between sensor outputs and PLC input modules must be verified to avoid signal mismatches. Regular maintenance, including lens cleaning and software updates, ensures long-term reliability.
In conclusion, the synergy between PLCs and laser sensors drives innovation in industrial automation. By following best practices in selection, wiring, and programming, engineers can unlock new levels of efficiency and accuracy. As Industry 4.0 evolves, this integration will continue to expand, incorporating IoT and AI for smarter, adaptive systems that redefine manufacturing landscapes.