Calibrating a profile laser sensor is a critical step in ensuring the accuracy, repeatability, and reliability of dimensional measurement and inspection systems across various industries, including automotive, electronics, and precision manufacturing. This process, often referred to as sensor commissioning or alignment, involves a series of systematic adjustments to optimize the sensor's performance for a specific application. A poorly calibrated sensor can lead to significant measurement errors, production defects, and costly downtime. This guide outlines the fundamental principles and a step-by-step methodology for effective profile laser sensor calibration.
Before initiating the calibration procedure, thorough preparation is essential. First, ensure the sensor is securely mounted in its final operational position. Vibration or movement post-calibration will invalidate the setup. The measurement environment should be stable, with controlled lighting to minimize ambient optical noise. The target object or a calibration artifact (e.g., a certified gauge block or a precision-machined master part) must be clean and placed within the sensor's specified measurement range (Z-axis) and field of view (X-axis). Power on the sensor and its associated controller or software interface, allowing sufficient warm-up time as per the manufacturer's specifications to stabilize internal electronics.
The core calibration process typically involves several key parameter adjustments. The primary goal is to align the laser plane accurately with the target surface and configure the sensor's internal processing for optimal data acquisition.
1. Focus and Laser Line Optimization: The initial step is adjusting the sensor's focus. The laser line projected onto the target should appear sharp, thin, and with uniform intensity across the entire field of view. Most sensors feature a manual focus ring or a software-controlled focus adjustment. A blurred or thick laser line reduces edge detection accuracy. Simultaneously, adjust the laser power or exposure time within the software to ensure the line is bright enough to be detected by the camera without causing saturation ("blooming") on highly reflective surfaces. The ideal setting provides a high-contrast image between the laser line and the background.
2. Coordinate System Alignment: This is arguably the most crucial step for accurate measurement. The sensor's internal 2D coordinate system (X-Z plane) must be aligned with the world coordinate system of the machine or conveyor. Misalignment causes skewed profile data. The standard method involves scanning a known flat reference surface or an artifact with a precise vertical edge. By analyzing the captured profile, you can determine angular offsets. Software tools usually provide "tilt" or "roll" correction functions to mathematically rotate the profile data until the reference surface appears perfectly horizontal or the vertical edge appears perfectly vertical. Some advanced sensors allow for mechanical adjustment of the sensor head itself for coarse alignment.
3. Setting the Reference (Zero) Point: Establish a spatial reference point for all subsequent measurements. This is often done by placing a calibration artifact of known height (e.g., a gauge block) at a specific location. In the software, you define this known height, thereby setting the Z=0 reference plane. All height measurements will be relative to this plane. For width or position measurements in the X-axis, a similar process using a known width artifact sets the X=0 point.
4. Configuring Measurement Tools and Filters: After spatial alignment, configure the specific measurement tools (e.g., edge detectors, gap/width tools, height tools) on the profile data. Set appropriate search windows and regions of interest (ROI) to ignore irrelevant parts of the scene. Apply data filtering judiciously. Temporal averaging (e.g., 3-5 profile averages) smooths out random noise. Median filters help eliminate outlier points from dust or minor surface imperfections. However, excessive filtering can introduce lag and obscure genuine surface features. The key is to use the minimum filtering required for stable readings.
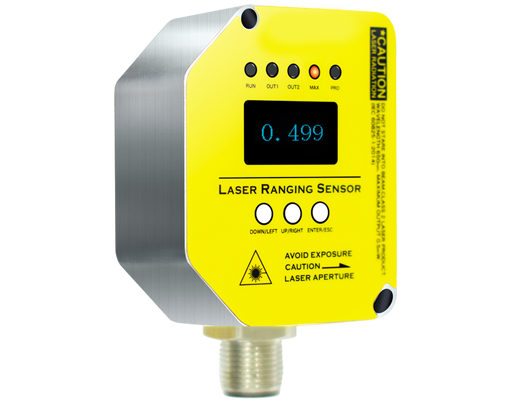
5. Validation and Repeatability Testing: Calibration is not complete without rigorous validation. Measure the calibration artifact multiple times to establish baseline accuracy. Then, perform a Gage Repeatability and Reproducibility (Gage R&R) study if possible. This involves taking multiple measurements of the same part by the same operator and different operators to quantify measurement variation. The results should fall within the tolerances required for your application. Document all calibration parameters, including laser power, exposure, focus position, alignment angles, and filter settings. This documentation is vital for audit trails and for restoring settings after a sensor reset or replacement.
Common challenges during calibration include dealing with highly reflective or dark surfaces, which may require adjusting laser power and exposure dynamically or using specialized sensor models. Vibrational environments necessitate faster exposure times and robust mechanical mounting. Always consult the sensor's user manual for model-specific features and recommended practices.
In conclusion, meticulous calibration transforms a profile laser sensor from a generic device into a precision measurement tool tailored to a specific task. By following a structured approach—focusing on mechanical stability, precise optical alignment, careful parameter tuning, and thorough validation—engineers can ensure their laser profiling systems deliver the high-fidelity data necessary for quality control, process monitoring, and robotic guidance, thereby maximizing return on investment and maintaining stringent production standards.