In the competitive landscape of modern manufacturing and processing industries, achieving unparalleled precision in quality control is not just an advantage—it’s a necessity. Among the array of advanced technologies driving this evolution, laser color sorting sensors stand out as a transformative force. These sophisticated devices harness the power of laser illumination and high-resolution spectral analysis to inspect, classify, and separate materials based on color and structural properties with extraordinary accuracy. Unlike traditional optical sorters that rely on broad-spectrum visible light, laser-based systems emit focused, coherent light at specific wavelengths. This allows for deeper material penetration and the detection of subtler color variations, surface defects, or compositional differences invisible to conventional cameras or the human eye.
The core mechanism involves projecting a laser beam onto the target material—be it agricultural products like rice or coffee beans, recycled plastics, minerals, or pharmaceutical granules. The sensor then captures the reflected or transmitted light spectrum. Advanced algorithms analyze this spectral signature in real-time, comparing it against predefined acceptance parameters. When a discrepancy is identified—such as a discolored seed, a foreign polymer type, or an impurity—the system triggers a precise ejection device, often using compressed air jets, to remove the defective item from the production line. This entire process occurs at remarkable speeds, with high-throughput systems capable of examining and sorting several tons of material per hour.
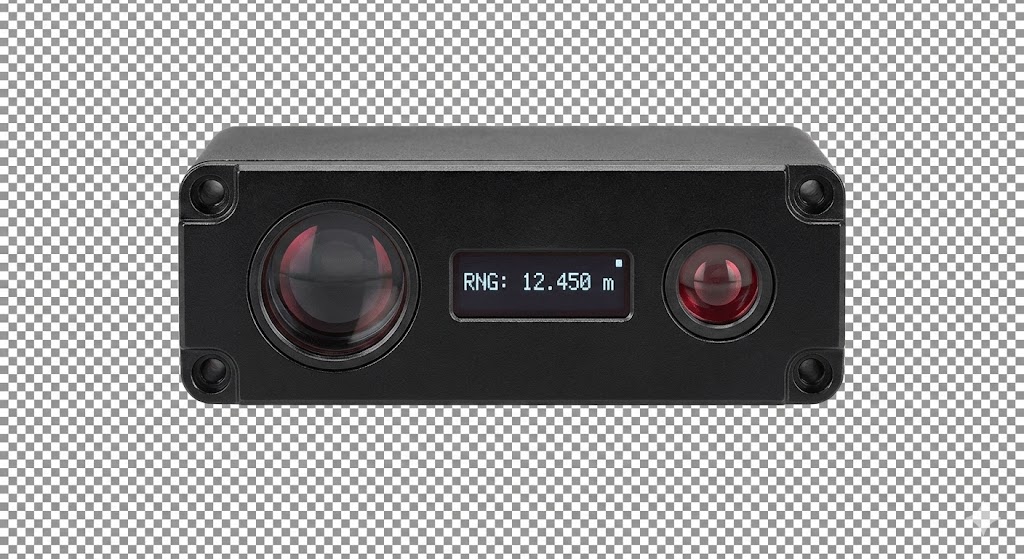
One of the paramount benefits of laser color sorting technology is its exceptional consistency and reliability. Human inspectors or basic camera systems can suffer from fatigue, subjective judgment, or limitations in lighting conditions. Laser sensors, however, deliver objective, repeatable measurements unaffected by ambient light fluctuations. This leads to a dramatic reduction in product waste, ensures compliance with stringent safety and quality standards, and significantly boosts overall yield. For instance, in the food industry, these sensors can meticulously remove aflatoxin-contaminated nuts or stones from grain streams, enhancing consumer safety. In recycling facilities, they enable precise separation of plastic types by color and polymer composition, driving efficiency in circular economies.
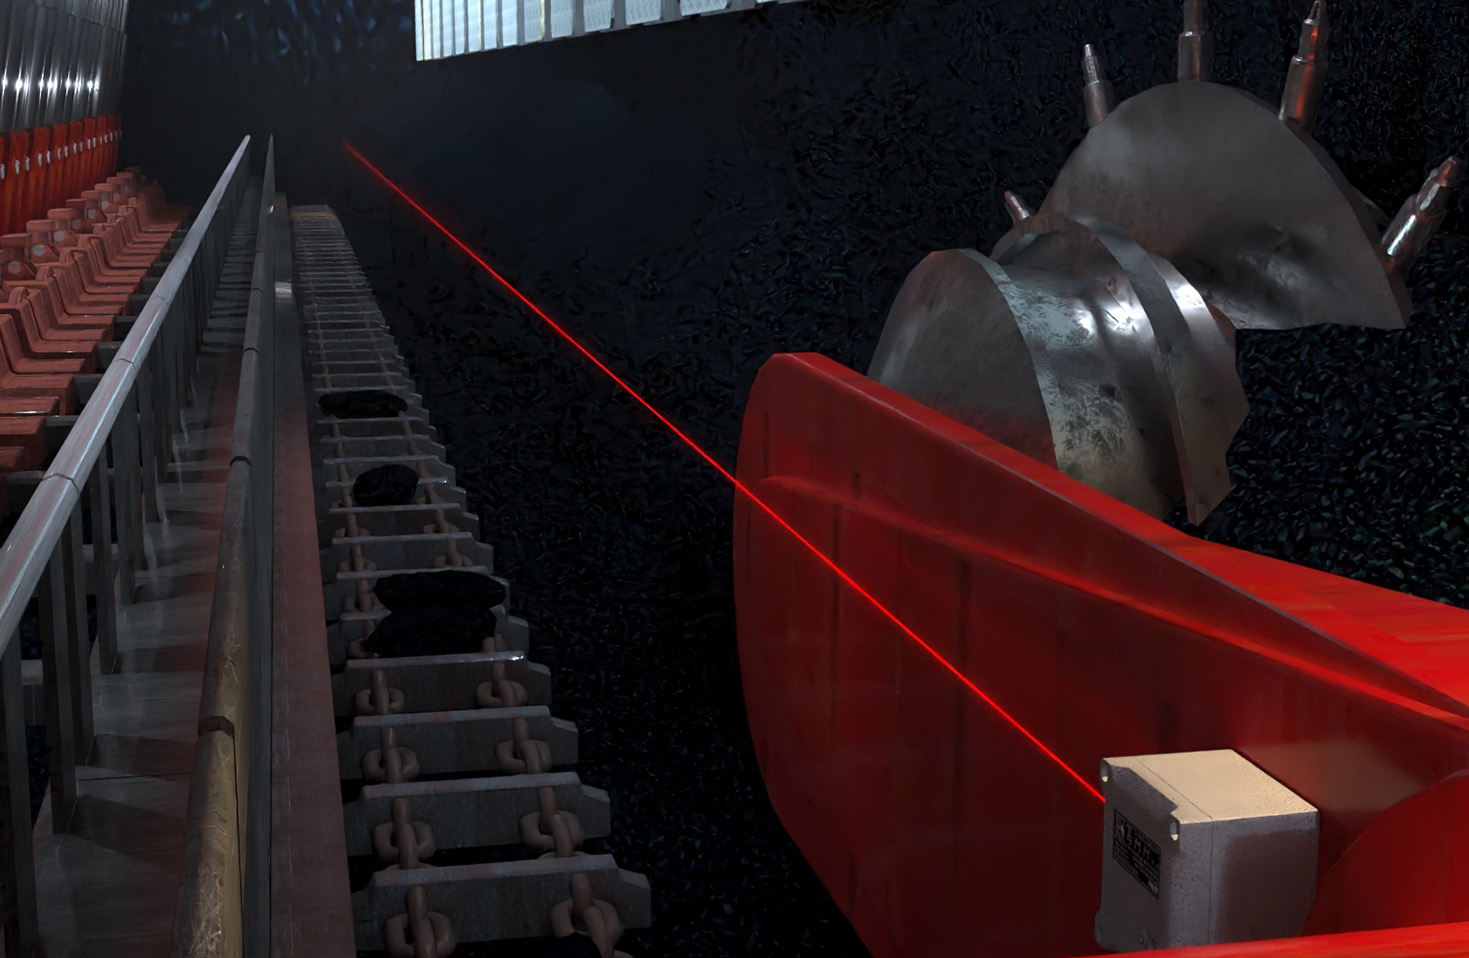
Furthermore, the adaptability of modern laser sorting sensors is noteworthy. They can be fine-tuned for a vast range of materials and specific defect types. Users can define custom sorting criteria through intuitive software interfaces, allowing the same hardware platform to switch between sorting green coffee beans by roast level and sorting industrial diamonds by clarity. Integration with Industry 4.0 frameworks is seamless, with sensors providing continuous data streams on sorting efficiency, defect rates, and production trends. This data empowers predictive maintenance and process optimization, contributing to smarter, more autonomous factories.
Despite the higher initial investment compared to conventional optical sorters, the return on investment is compelling. The reduction in labor costs, the minimization of high-value material loss, and the ability to command premium prices for consistently superior products justify the capital expenditure. Moreover, the technology’s precision reduces the need for downstream reprocessing, saving energy and additional operational costs.
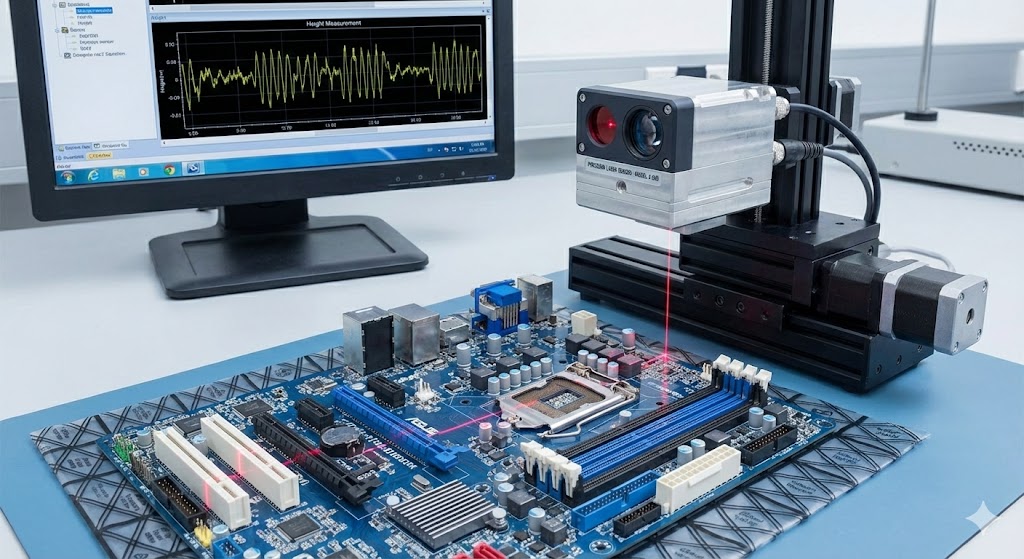
In conclusion, laser color sorting sensors represent a significant leap forward in automated quality assurance. By delivering unmatched accuracy, speed, and flexibility, they are becoming an indispensable tool across diverse sectors—from food and mining to plastics and pharmaceuticals. As sensor technology and machine learning algorithms continue to advance, we can anticipate even greater capabilities, further solidifying their role in building more efficient, sustainable, and quality-driven industrial operations. Their impact extends beyond mere sorting; they are fundamental enablers of higher standards, greater profitability, and enhanced resource utilization in the global supply chain.